Summary
An industrial facility may require a reliable diesel transfer system capable of supplying multiple burners from a remote bulk fuel storage tank. In this hypothetical scenario, Anglo Nordic equipment is selected to support fuel transfer, fuel conditioning, pressure control and leak detection within a critical heating application.
Project Overview
- Industry: Industrial Heating
- Application: Industrial Boiler House
- Fuel: Diesel
- Transfer Duty: 500 l/h
- Burners Served: Three diesel-fired burners
- Storage Arrangement: Client-supplied bunded fuel tank
- Transfer Distance: 100m
- Vertical Lift: 10m
Project Requirements
- Transfer diesel over 100 metres with a 10-metre vertical lift.
- Supply three diesel-fired burners.
- Deliver approximately 500 l/h.
- Provide duty/standby resilience.
- Maintain fuel quality during storage.
- Regulate fuel pressure to downstream equipment.
- Detect fuel leaks quickly and effectively.
The Challenge
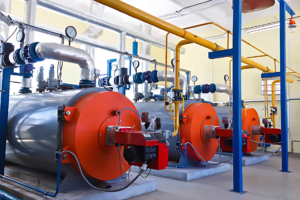
Industrial boiler houses often rely on a consistent fuel supply to maintain heating operations and process continuity. With fuel storage located remotely from the boiler plant, the fuel handling system would need to provide reliable fuel delivery whilst maintaining fuel quality and supporting safe operation.
Equipment and Solution
In this proposed arrangement, diesel would be transferred from a client-supplied bunded storage tank using an Inpro GP-500 GE Twin Pump Transfer Unit. The duty/standby pump arrangement could provide operational resilience, whilst integrated filtration, monitoring and isolation components would support dependable fuel delivery.
To maintain fuel quality, a dedicated MiniSAFA Fuel Conditioning System could continuously recirculate and condition stored fuel, helping to remove water and contaminants that may affect combustion performance.
Fuel pressure could be regulated using an HP Pressure Reducing Valve, helping maintain a stable downstream fuel supply whilst protecting burner equipment from pressure fluctuations.
An Inpro Leak Detection System could be incorporated within designated containment areas to provide early indication of fuel leakage and support safe system operation.
The proposed system would be designed to maintain fuel quality, provide stable operating conditions and support reliable fuel delivery to all three burners.
Equipment Breakdown
Inpro GP-500 GE Twin Pump Transfer Unit
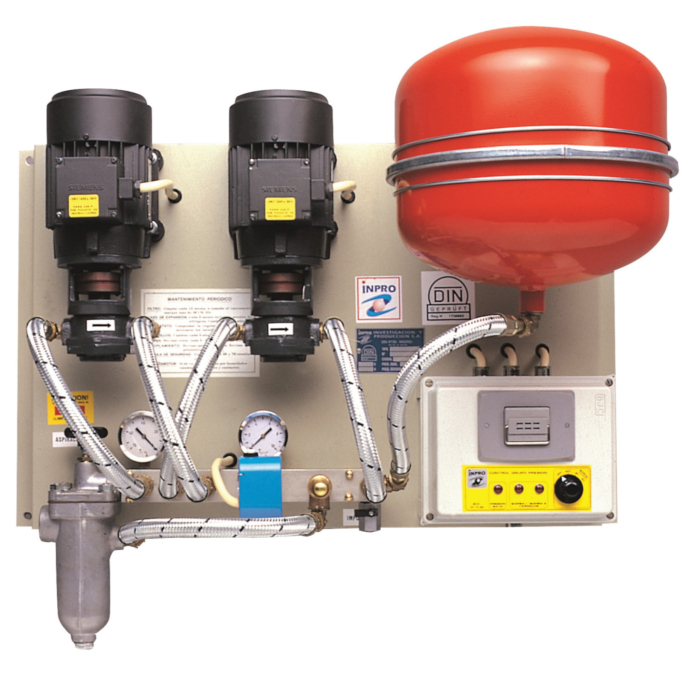
- Flow rate: 500 l/h
- Twin duty/standby pump arrangement
- Integrated filtration and monitoring
- Manufactured to DIN EN 12514-1
MiniSAFA Fuel Polishing System
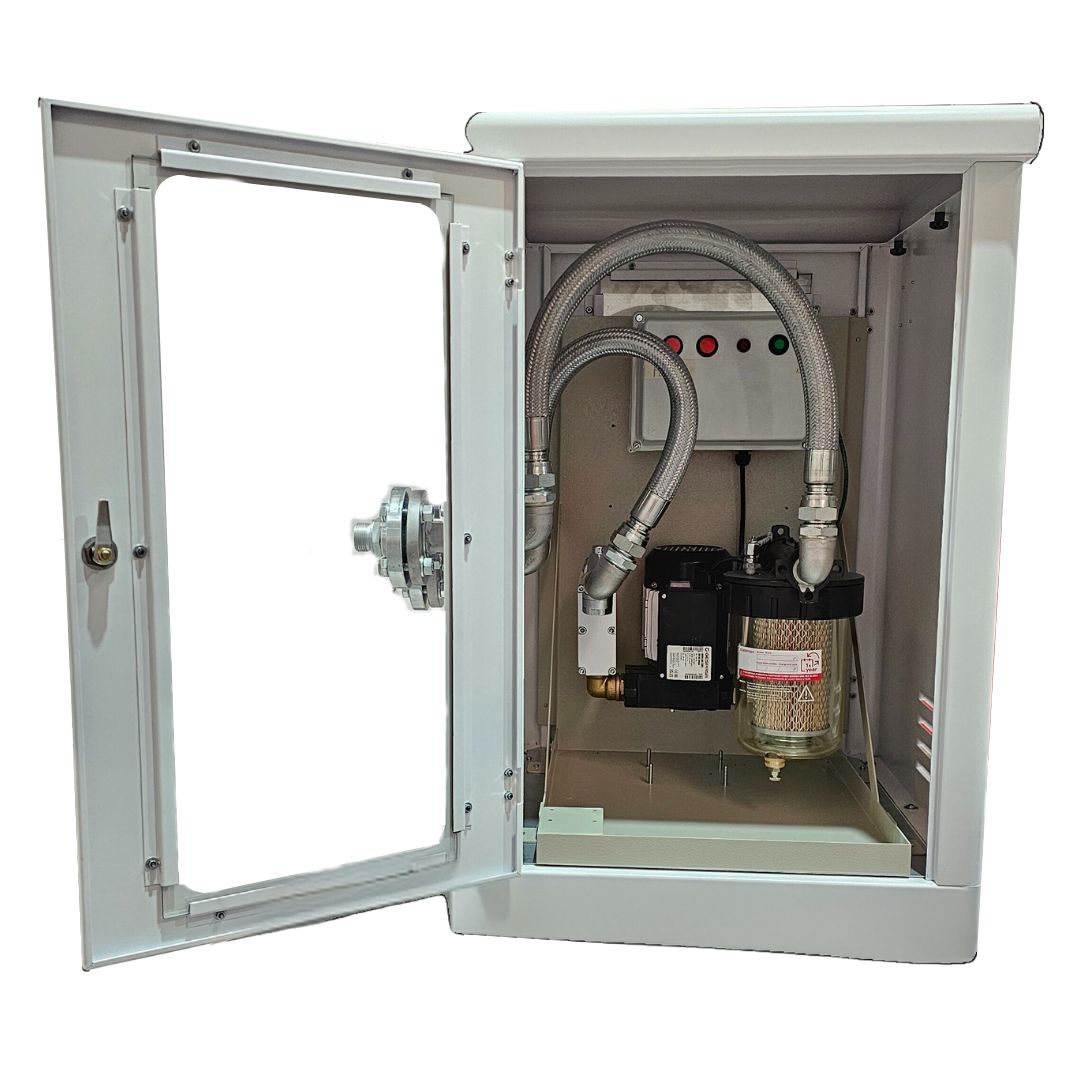
- Recommended for tanks up to 50,000 litres
- Nominal flow: 40 l/min
- Maximum flow: 50 l/min
- Fuel conditioning, filtration and water separation
HP Pressure Reducing Valve
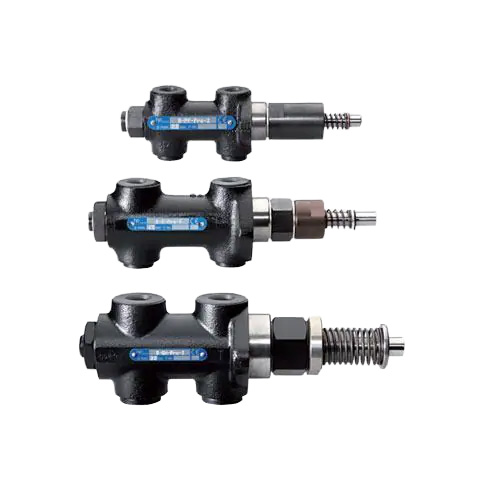
- Connection sizes: G 3/4″ and G 1″
- Maximum inlet pressure: 25 bar
- Adjustable outlet pressure options from 0.5-3 bar up to 0.5-10 bar
- Diaphragm-operated pressure regulator
Inpro Leak Detection System

- Infrared leak detection technology
- Visual indication and relay output
- Suitable for leak collection trays and containment areas
Equipment List
- Inpro GP-500 GE Twin Pump Transfer Unit
- MiniSAFA Fuel Conditioning System
- HP Pressure Reducing Valve
- Inpro Leak Detection System
Get in touch today
Whether supporting industrial boiler houses, district heating schemes or large-scale commercial heating installations, Anglo Nordic provides fuel transfer, conditioning and monitoring solutions that can be configured to suit a wide range of industrial heating applications.